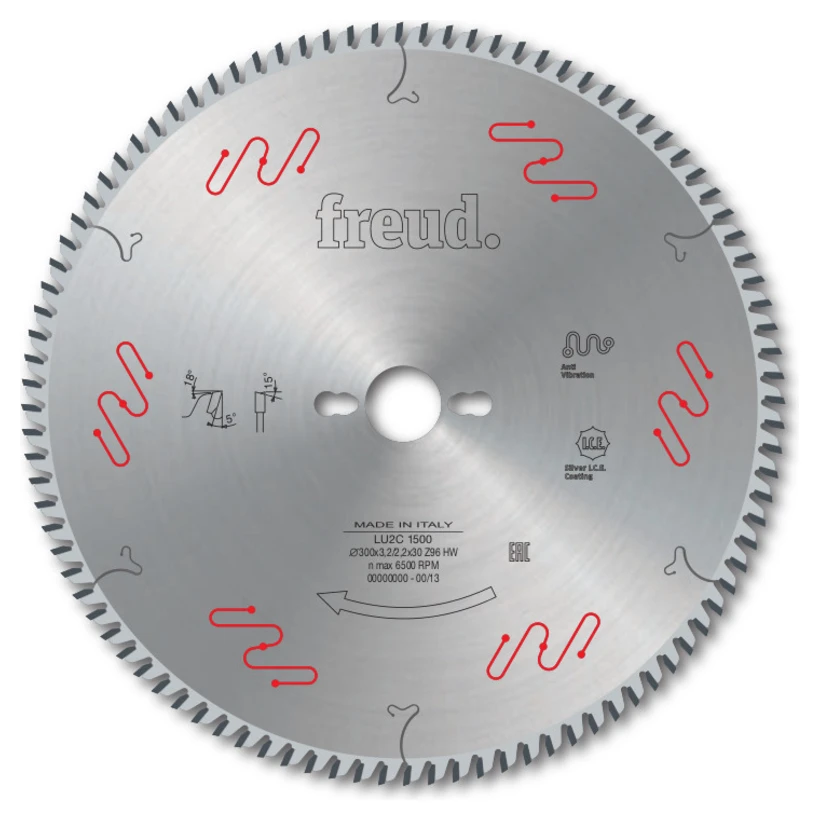
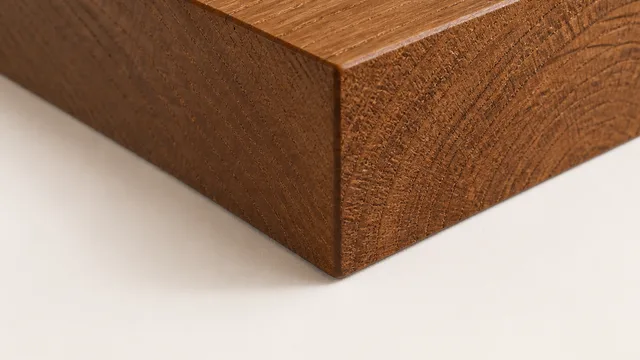
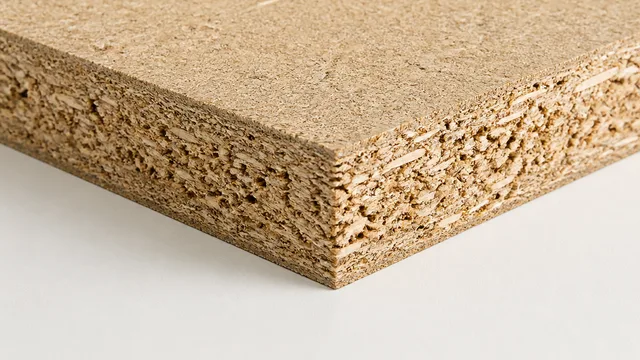
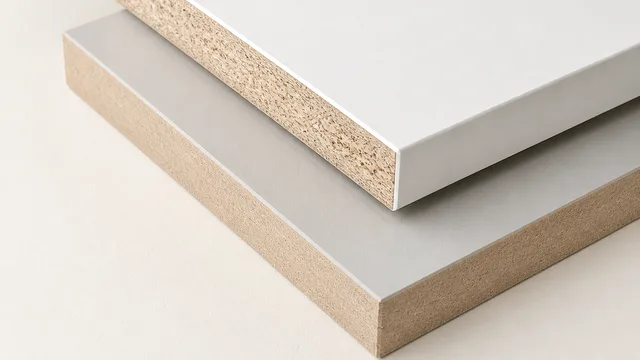
LU2C specialises in crosscutting, where panel edges are most exposed to chipping. Its 25 configurations use the highest tooth counts in the LU2 range, from 48 teeth at 150 mm to 168 teeth at 600 mm. The restrained 5° hook angle supports a controlled cutting action on laminated surfaces and thermoplastic composites.
Application
Crosscutting
Eccellente
Material
Softwood
Suitable
Material
Hardwood
Suitable
Material
Chipboard
Suitable
Material
Laminated MDF
Suitable
Material
Thermoplastic composites
Suitable
Technical note
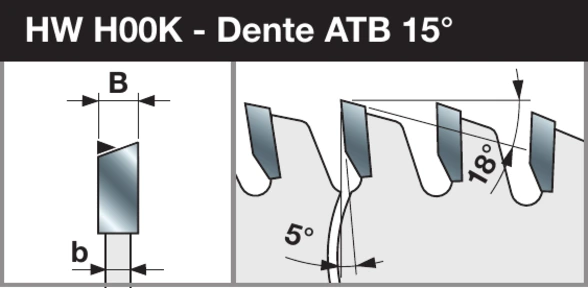
H00K carbide, 15° ATB tooth geometry and positive 5° hook angle. Blades from 230 mm have anti-vibration slots. Use a more controlled feed rate than with a universal blade; forcing the cut creates heat without improving finish.
Compatibility at a glance
Machines and materials
01 Compatible machines
Squaring sawsHand-held circular saws
02 Suitable materials
Softwood
Legno massiccio
Hardwood
Legno massiccio
Chipboard
Pannello a base legno
Laminated MDF
Pannello rivestito
Thermoplastic composites
Materiale composito
Always check the pin-hole pattern
Technical configuration
Tooth geometry and technologies
Shared family specifications, kept separate from the dimensions of each individual code.
Once LU2C has been identified, the exact product code depends on the machine requirements. The portal keeps these two decisions separate.
1
Check the machine
Permitted diameter, bore and pin holes.
2
Confirm the application
Crosscutting.
3
Choose the variant
Kerf, plate thickness and tooth count.
4
Check the operating parameters
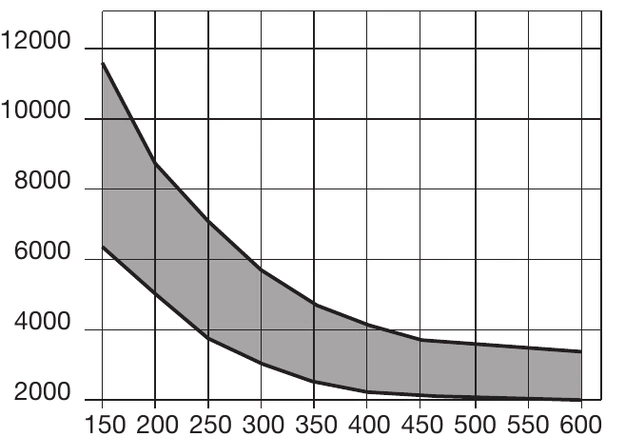
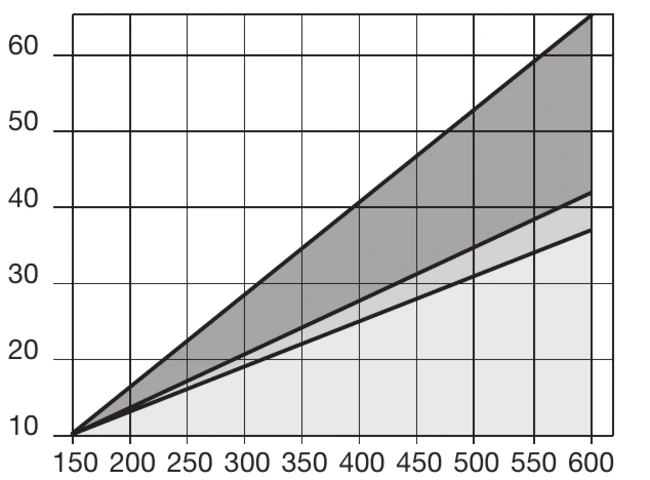
Speed and cutting height according to the family charts.
Frequently asked questions
Questions about the LU2C family
Quick answers for checking the application, compatibility and operating parameters before selecting a product code.
01What is the LU2C family designed for?
LU2C is designed for Crosscutting. Its suitability must be checked against the material, machine and exact variant specifications.
02Which materials can LU2C cut?
The family is specified for Softwood, Hardwood, Chipboard, Laminated MDF, Thermoplastic composites. Material density, coating, thickness and condition can affect the resulting edge quality. For LU2C, verify the selected reference within its 150–600 mm diameter and 48–168-tooth range.
03Which machines can use LU2C blades?
The catalogue specifies Squaring saws, Hand-held circular saws. Before fitting, check diameter, bore, flange or pin-hole pattern and the permitted maximum speed. For LU2C, verify the selected reference within its 150–600 mm diameter and 48–168-tooth range.
04What tooth geometry does LU2C use?
The family uses ATB 15° tooth geometry. Refer to the technical note for the carbide grade and hook angle. For LU2C, verify the selected reference within its 150–600 mm diameter and 48–168-tooth range.
05How many LU2C variants are available?
There are 25 variants, with diameters from 150 to 600 mm, bores from 20 to 40 mm and tooth counts from 48 to 168. For LU2C, verify the selected reference within its 150–600 mm diameter and 48–168-tooth range.
06How do I select the correct LU2C code?
For LU2C, start with the machine bore (20–40 mm) and the required diameter (150–600 mm). Then select within the available 48–168-tooth range by comparing kerf, plate thickness and any pin holes or keyways.
07At what speed should a LU2C blade run?
The correct speed for an LU2C blade depends on the selected diameter, which ranges from 150 to 600 mm, and on the machine. Never exceed the lower of the maximum RPM marked on that blade and the machine manufacturer’s limit.
08Can LU2C blades be resharpened?
A specialist can assess and resharpen the ATB carbide teeth used by LU2C, provided the blade body is undamaged. The original geometry, angles and balance must be preserved; the number of possible services depends on the condition of the selected reference.
Guides
Guides related to this blade family
The catalogue starts with the tool; the guides start with the cutting problem. If you are still choosing, read these first.