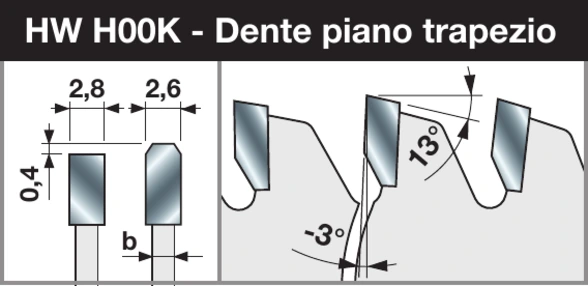
Dente piano trapezio
H00K carbide, TCG tooth geometry and negative -3° hook angle.
Professional circular saw bladesFreud
Two Freud blades for cutting Plexiglas and plastic sheets on squaring saws, table saws and hand-held circular saws, in 250 and 300 mm diameters.
Application
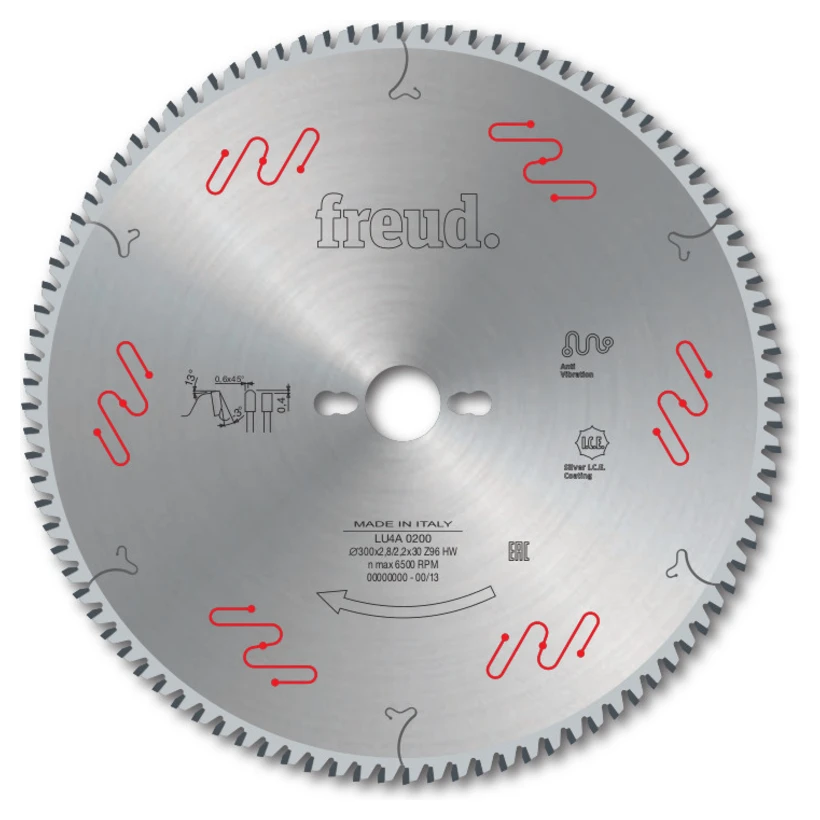
LU4A is dedicated to Plexiglas and plastic sheet: a 250 mm Z80 and a 300 mm Z96 blade, both with a 30 mm bore and 2.8 mm kerf. Its dense TCG tooth geometry and negative -3° hook angle produce a controlled scraping action rather than aggressively pulling into the material.
Technical note
H00K carbide, TCG tooth geometry and -3° hook angle. Freud recommends approximately 30 mm blade projection above the workpiece. The blade body has anti-vibration slots and FT01 is the specified pin-hole pattern.
Compatibility at a glance
01 Compatible machines
02 Suitable materials
Always check the pin-hole pattern
Technical configuration
Shared family specifications, kept separate from the dimensions of each individual code.
H00K carbide, TCG tooth geometry and negative -3° hook angle.
Specially formulated carbide tips for durability and cutting quality.
Coating designed to reduce friction, heat and material build-up.
Technology designed to reduce vibration and noise.
Operating parameters
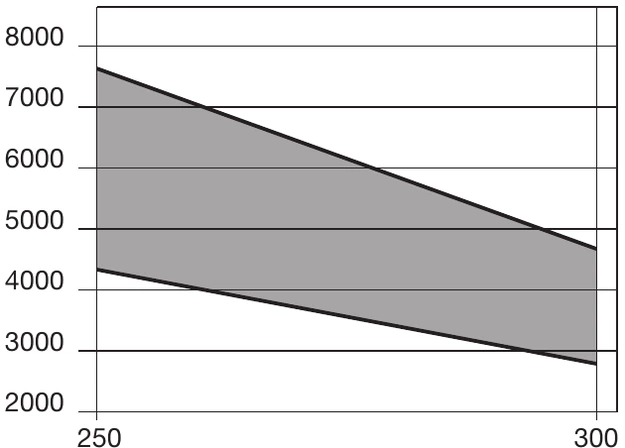
The chart shows how the recommended speed changes across the LU4A range.
Rotational speed
The actual speed must remain within the limits of both the blade and the machine.
Essential check: before fitting the blade, check its diameter, bore, pin-hole pattern, direction of rotation and the maximum RPM marked on the blade.
Dimensional selector
Filter the variants by the two key dimensions, then compare kerf, plate thickness, tooth count and pin-hole patterns.
| Code | Ø mm | Kerf B | Plate b | Bore d | Teeth Z | NL / KN | Article no. |
|---|---|---|---|---|---|---|---|
| LU4A0100 | 250 | 2.8 | 2.2 | 30 | 80 | FT01 | F03FS05163 |
| LU4A0200 | 300 | 2.8 | 2.2 | 30 | 96 | FT01 | F03FS05165 |
Before choosing
Once LU4A has been identified, the exact product code depends on the machine requirements. The portal keeps these two decisions separate.
Permitted diameter, bore and pin holes.
Cutting plastic materials.
Kerf, plate thickness and tooth count.
Speed and cutting height according to the family charts.
Frequently asked questions
Quick answers for checking the application, compatibility and operating parameters before selecting a product code.
LU4A is designed for cutting Plexiglas and other plastic sheet materials. Always verify the exact material, machine and variant parameters.
The catalogue specifies Plexiglas and plastic materials. Polymer type, surface condition and thickness influence the result as much as blade selection. For LU4A, verify the selected reference within its 250–300 mm diameter and 80–96-tooth range.
LU4A is intended for squaring saws, table saws and hand-held circular saws. Check the bore, flange, pin-hole pattern and maximum speed before fitting.
It uses H00K carbide, TCG tooth geometry and a negative -3° hook angle. For LU4A, verify the selected reference within its 250–300 mm diameter and 80–96-tooth range.
There are two: 250 mm with 80 teeth and 300 mm with 96 teeth. Both use a 30 mm bore. For LU4A, verify the selected reference within its 250–300 mm diameter and 80–96-tooth range.
A positive angle can grab and lift plastic. The -3° angle creates a controlled scraping action that helps keep Plexiglas edges clean and reduces chipping. For LU4A, verify the selected reference within its 250–300 mm diameter and 80–96-tooth range.
The catalogue recommends approximately 30 mm. Too little projection increases tangential rubbing, heat and the risk of melted swarf adhering to the edge. For LU4A, verify the selected reference within its 250–300 mm diameter and 80–96-tooth range.
A specialist can resharpen the carbide teeth while preserving tooth geometry, angles and balance, after checking the blade body for damage. For LU4A, verify the selected reference within its 250–300 mm diameter and 80–96-tooth range.
Guides
The catalogue starts with the tool; the guides start with the cutting problem. If you are still choosing, read these first.
Maximum rpm is based on peripheral speed, not an arbitrary table. Some blade families have much lower specific limits.
Open guide 5 min readThe only material group in which the cut can literally fuse together again behind the blade. The main enemy is not hardness but heat.
Open guide