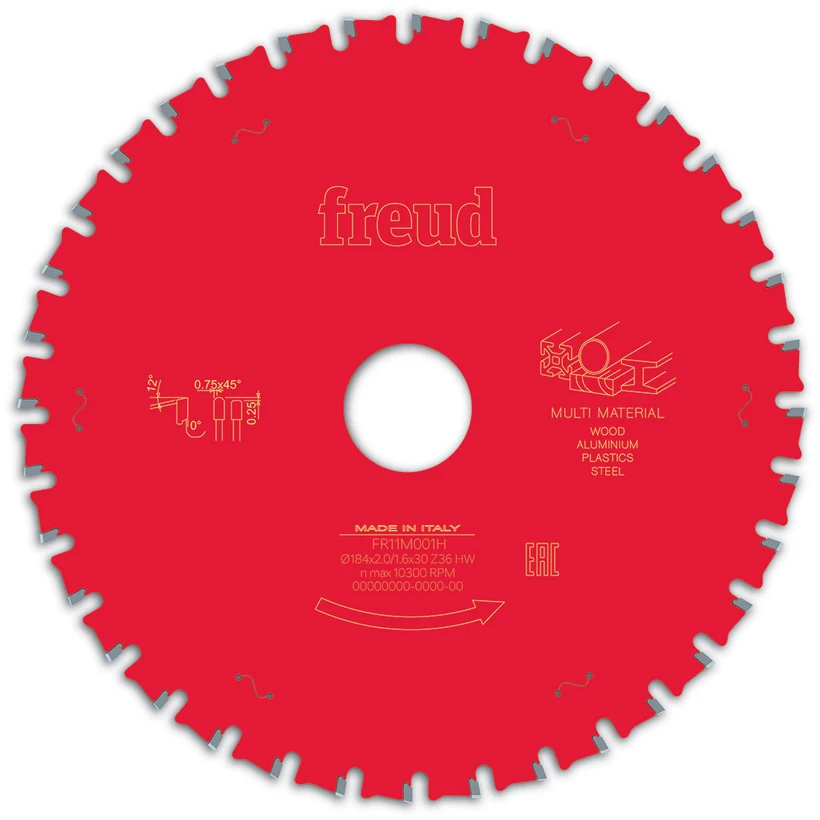
The FRMPI range includes 4 configurations, with diameters from 160 to 230 mm, bore sizes from 20 to 30 mm and tooth counts from 30 to 44. Use the dimensional selector to identify compatible codes, then compare kerf, plate thickness and pin-hole pattern.
Application
Cutting plastic materials
Suitable
Application
Cutting non-ferrous metals
Suitable
Application
Cutting ferrous metals
Suitable
Material
MDF
Suitable
Material
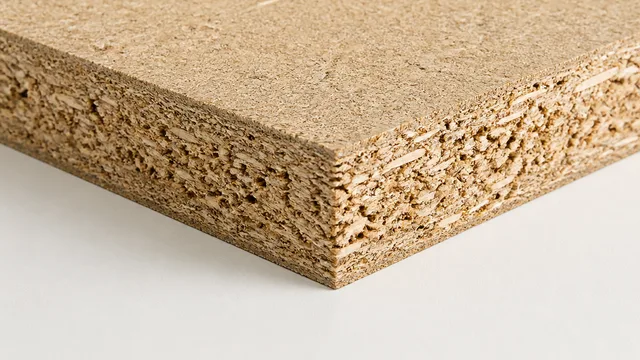
Chipboard
Suitable
Material
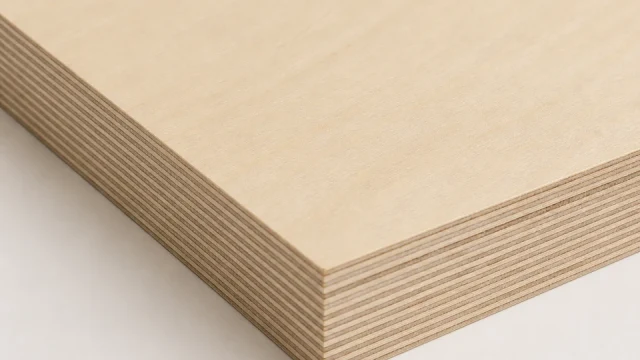
Plywood
Suitable
Material
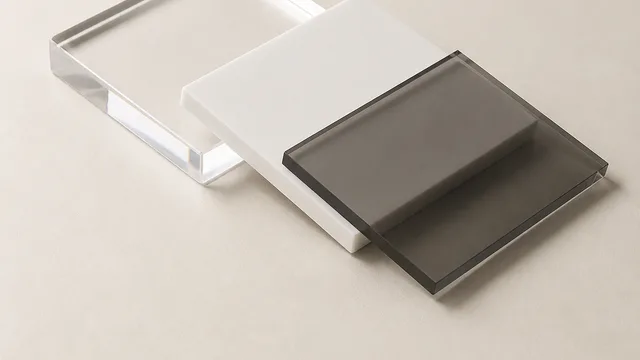
Plastic materials
Suitable
Material
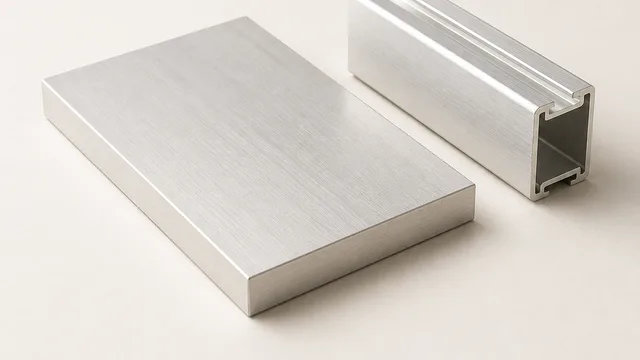
Aluminium
Suitable
Material
Copper and brass
Suitable
Material
Thin-gauge steel
Suitable
Technical note
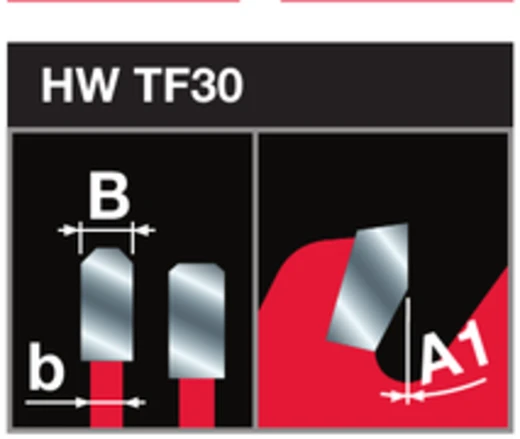
HW TF30 carbide, HLTCG tooth geometry, a 0° hook angle. Check blade diameter, bore, flange or pin-hole pattern and maximum RPM against the machine specifications before fitting.
Compatibility at a glance
Machines and materials
01 Compatible machines
Hand-held circular sawsPlunge saws
02 Suitable materials
MDF
Pannello a base legno
Chipboard
Pannello a base legno
Plywood
Pannello di legno
Plastic materials
Materiale plastico
Aluminium
Metallo non ferroso
Copper and brass
Metallo non ferroso
Thin-gauge steel
Profilo in acciaio
Always check the pin-hole pattern
Technical configuration
Tooth geometry and technologies
Shared family specifications, kept separate from the dimensions of each individual code.
HW HW TF300°
HLTCG
HW TF30 carbide, HLTCG tooth geometry.
TiCo Carbide
Specially formulated carbide tips for durability and cutting quality.
Perma-SHIELD
Technology used across this blade family.
Anti-vibration
Technology designed to reduce vibration and noise.
Dimensional selector
Find the correct product code
Filter the variants by the two key dimensions, then compare kerf, plate thickness, tooth count and pin-hole patterns.
4 variants found
D diameterB kerfb plate thicknessd boreZ teeth
Code
Ø mm
Kerf B
Plate b
Bore d
Teeth Z
Tooth
Article no.
FR06M001H
160
2
1.6
20
30
HLTCG 0°
F03FS10114
FR11M001H
184
2
1.6
30
36
HLTCG 0°
F03FS10113
FR13M001H
190
2
1.6
30
38
HLTCG 0°
F03FS10041
FR19M001H
230
2.4
2
30
44
HLTCG 0°
F03FS10042
Before choosing
The blade family is only the first step
Once FRMPI has been identified, the exact product code depends on the machine requirements. The portal keeps these two decisions separate.
Speed and cutting height according to the family charts.
Frequently asked questions
Questions about the FRMPI family
Quick answers for checking the application, compatibility and operating parameters before selecting a product code.
01What is the FRMPI family designed for?
FRMPI is designed for Cutting plastic materials and Cutting non-ferrous metals and Cutting ferrous metals. Its suitability must be checked against the material, machine and exact variant specifications.
02Which materials can FRMPI cut?
The family is specified for MDF, Chipboard, Plywood, Plastic materials, Aluminium, Copper and brass, Thin-gauge steel. Material density, coating, thickness and condition can affect the resulting edge quality. For FRMPI, verify the selected reference within its 160–230 mm diameter and 30–44-tooth range.
03Which machines can use FRMPI blades?
The catalogue specifies Hand-held circular saws, Plunge saws. Before fitting, check diameter, bore, flange or pin-hole pattern and the permitted maximum speed. For FRMPI, verify the selected reference within its 160–230 mm diameter and 30–44-tooth range.
04What tooth geometry does FRMPI use?
The family uses HLTCG tooth geometry. Refer to the technical note for the carbide grade and hook angle. For FRMPI, verify the selected reference within its 160–230 mm diameter and 30–44-tooth range.
05How many FRMPI variants are available?
There are 4 variants, with diameters from 160 to 230 mm, bores from 20 to 30 mm and tooth counts from 30 to 44. For FRMPI, verify the selected reference within its 160–230 mm diameter and 30–44-tooth range.
06How do I select the correct FRMPI code?
For FRMPI, start with the machine bore (20–30 mm) and the required diameter (160–230 mm). Then select within the available 30–44-tooth range by comparing kerf, plate thickness and any pin holes or keyways.
07At what speed should a FRMPI blade run?
The correct speed for an FRMPI blade depends on the selected diameter, which ranges from 160 to 230 mm, and on the machine. Never exceed the lower of the maximum RPM marked on that blade and the machine manufacturer’s limit.
08Can FRMPI blades be resharpened?
A specialist can assess and resharpen the HLTCG carbide teeth used by FRMPI, provided the blade body is undamaged. The original geometry, angles and balance must be preserved; the number of possible services depends on the condition of the selected reference.
Guides
Guides related to this blade family
The catalogue starts with the tool; the guides start with the cutting problem. If you are still choosing, read these first.